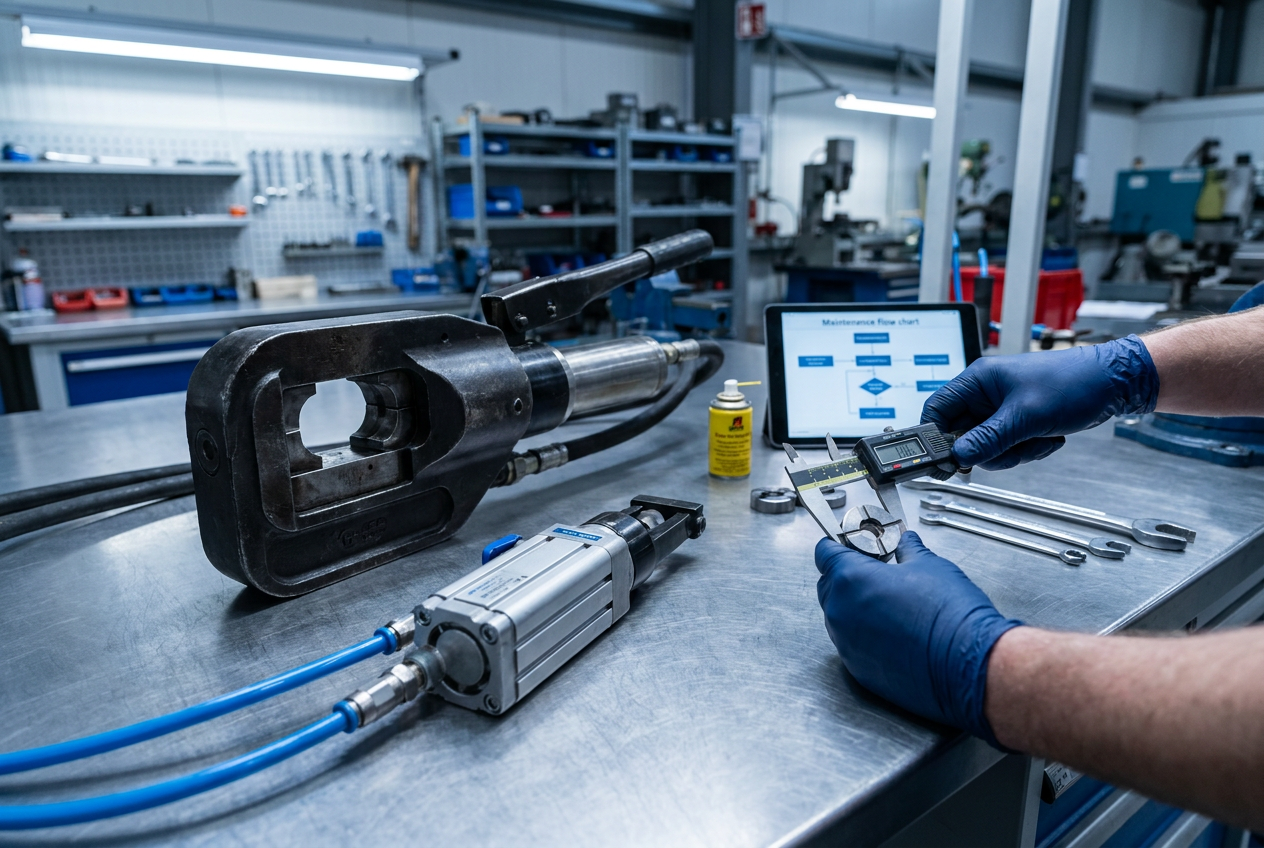
Why Pneumatic and Hydraulic Crimpers Fail Without a Maintenance Schedule
Unscheduled downtime on the production floor often traces back to neglected pneumatic and hydraulic crimpers. In aerospace wire harness manufacturing, high-cycle bench tools face severe mechanical loading. Without structured crimp tool preventive maintenance, microscopic die wear, hydraulic fluid contamination, and pressure seal degradation will compromise tensile strength long before an outright stall occurs.
Consider a pneumatic bench press terminating 22-AWG (American Wire Gauge) contacts in an MRO environment. If particulate accumulation restricts the air cylinder’s forward stroke, the cycle fails to reach terminal bottom-dead-center. You end up with under-crimped barrels, failing pull tests, and costly lot rejections during quality audits. Proactive scheduling eliminates these variables.
Establishing a Baseline: Tool Inventory, Documentation, and Specifications
You cannot protect what you do not catalog. Start your crimp tool preventive maintenance program by creating an exhaustive asset database. Record the manufacturer serial number, pneumatic pressure ratings, hydraulic fluid capacities, and specific die-set compatibility for every benchtop unit. Link each asset directly to its OEM maintenance manual and military specification requirements, such as SAE AS22520. Assign a unique barcode to every crimper to track cycle counts on the shop floor. Without this precise baseline, technicians rely on guesswork, which inevitably leads to out-of-tolerance aerospace wire harnesses and costly audit non-conformances during compliance reviews.
Daily and Pre-Shift Checks for Pneumatic and Hydraulic Crimpers
Before releasing a pneumatic or hydraulic crimper to the shop floor, your operators must execute a strict two-minute pre-shift inspection. Inspect the hydraulic fluid lines for micro-fractures, weeping fittings, and pressure drops that compromise the specified crimp force. For pneumatic units, check the inline filter-regulator-lubricator unit; drain any accumulated condensation from the bowl to prevent moisture ingress into internal valves. Visually inspect the die faces for copper shearing debris, plating flaking, or micro-cracks along the radius. Cycle the machine once with a scrap terminal to verify complete die retraction and cycle-abort mechanism engagement before processing flight-critical wire bundles.
Weekly and Monthly Preventive Maintenance Tasks
Transitioning past daily visual checks, your weekly protocols must target mechanical fatigue and fluid integrity. Every 50 operating hours, flush pneumatic moisture traps and inspect hydraulic lines for micro-abrasions caused by continuous bench articulation.
Monthly demands a deeper teardown. Remove the crimp die sets and clean residual copper shavings or plating flakes from the nest pockets using isopropyl alcohol and a brass pick. Apply a thin film of MIL-PRF-23827 grease to sliding ram surfaces. For hydraulic units, pull a fluid sample to check for particulate contamination that accelerates internal seal wear and causes pressure drops during the crimp cycle.
Calibration Intervals, Pull Testing, and Documentation Requirements
Execute destructive pull testing every 500 cycles to verify mechanical integrity against SAE AS22520 specifications. Mount terminal samples directly to your digital force gauge, maintaining a constant pull rate of one inch per minute until tensile failure occurs. Log exact breaking loads in your Statistical Process Control database immediately.
Recalibrate pneumatic rams and hydraulic pumps annually, or strictly after 10,000 actuation cycles. Send tooling to an ISO/IEC 17025 accredited lab for traceable verification. Archive all calibration certificates and corrective action logs for the lifetime of the wire harness assembly to satisfy FAA process compliance audits.
Common Failure Modes and Their Preventive Actions
Pneumatic crimper mis-strikes typically originate from contaminated air lines. If your cycle rate slows or the ram stalls mid-stroke, inspect the internal air cylinder seals for scoring caused by moisture. Install a refrigerated desiccant dryer upstream to eliminate particulate intrusion.
For hydraulic bench units, erratic pressure drops point to bypass valve contamination. Flush the hydraulic circuit and replace degraded O-rings annually to maintain consistent tonnage delivery. If die nests develop micro-fractures along the crimp radius, immediately quarantine the tooling. These stress cracks stem from excessive cycle force or improper die-to-frame alignment, directly threatening terminal tensile strength.
Building the Schedule: Roles, Triggers, and Recordkeeping
Assign clear responsibilities to keep your crimp tool preventive maintenance program running without friction. Operators execute daily pre-shift checks, while certified tool crib technicians handle weekly fluid analysis and pneumatic line purging. Quality assurance maintains oversight by auditing compliance logs monthly.
Establish dual maintenance triggers based on both calendar intervals and cycle counts tracked via digital counters on your hydraulic pumps. Tie every service action directly to an auditable electronic or physical asset tag. When an FAA or ISO auditor requests proof of compliance, your records must instantly display complete maintenance histories, calibration certificates, and pull-test data for every active crimper.
Maintenance Schedule Template and Reference Table
Implement this matrix to standardize your crimp tool preventive maintenance intervals across production and MRO lines.
| Interval | Core Task | Acceptance Criteria |
|---|---|---|
| Pre-Shift | Inspect dies, air lines, and fluid levels | Zero scoring on indenters; dry fittings |
| Weekly | Clean scrap buildup; check pneumatic lubricator | Unrestricted ram travel; clean oil bowl |
| Monthly | Verify hydraulic pressure relief settings | Relief triggers within $\pm 2%$ of spec |
| Annual | Full calibration and certification trace | Meets SAE AS22520 tensile pull requirements |
Adhering to this structured framework eliminates guesswork, protects mission-critical wire harnesses, and ensures unwavering compliance during quality audits.
Frequently Asked Questions
What triggers the need to initiate a crimp tool preventive maintenance program?
Facilities should catalog all pneumatic and hydraulic crimpers into an asset database before experiencing production bottlenecks or equipment failures. Establishing this baseline inventory ensures every high-cycle bench tool receives tracked servicing according to manufacturer specifications.
How often should operators inspect hydraulic fluid lines during production shifts?
Operators must perform a brief visual check of the hydraulic lines before releasing any crimper to the shop floor. This pre-shift assessment catches micro-fractures and weeping fittings early, preventing sudden pressure drops during active manufacturing cycles.
Why are destructive pull tests required for mechanical integrity verification?
Executing destructive pull tests every 500 cycles ensures that terminal crimps meet rigorous SAE AS22520 performance standards. Mounting samples to a digital force gauge at a controlled pull rate validates that the tool’s mechanical output hasn’t degraded under heavy production loads.
What causes pneumatic crimpers to experience ram stalls or slow cycle rates?
Sluggish performance or mid-stroke stalls usually point to internal air cylinder seal damage from moisture-contaminated air lines. Installing a refrigerated desiccant dryer upstream effectively stops this internal scoring and keeps pneumatic components operating smoothly.
Who is responsible for carrying out the various maintenance tasks on the shop floor?
Maintenance duties are shared based on technical complexity to maximize efficiency and safety. Operators handle fast pre-shift visual checks, while certified tool crib technicians manage deeper interventions like weekly fluid analyses and internal pneumatic servicing.