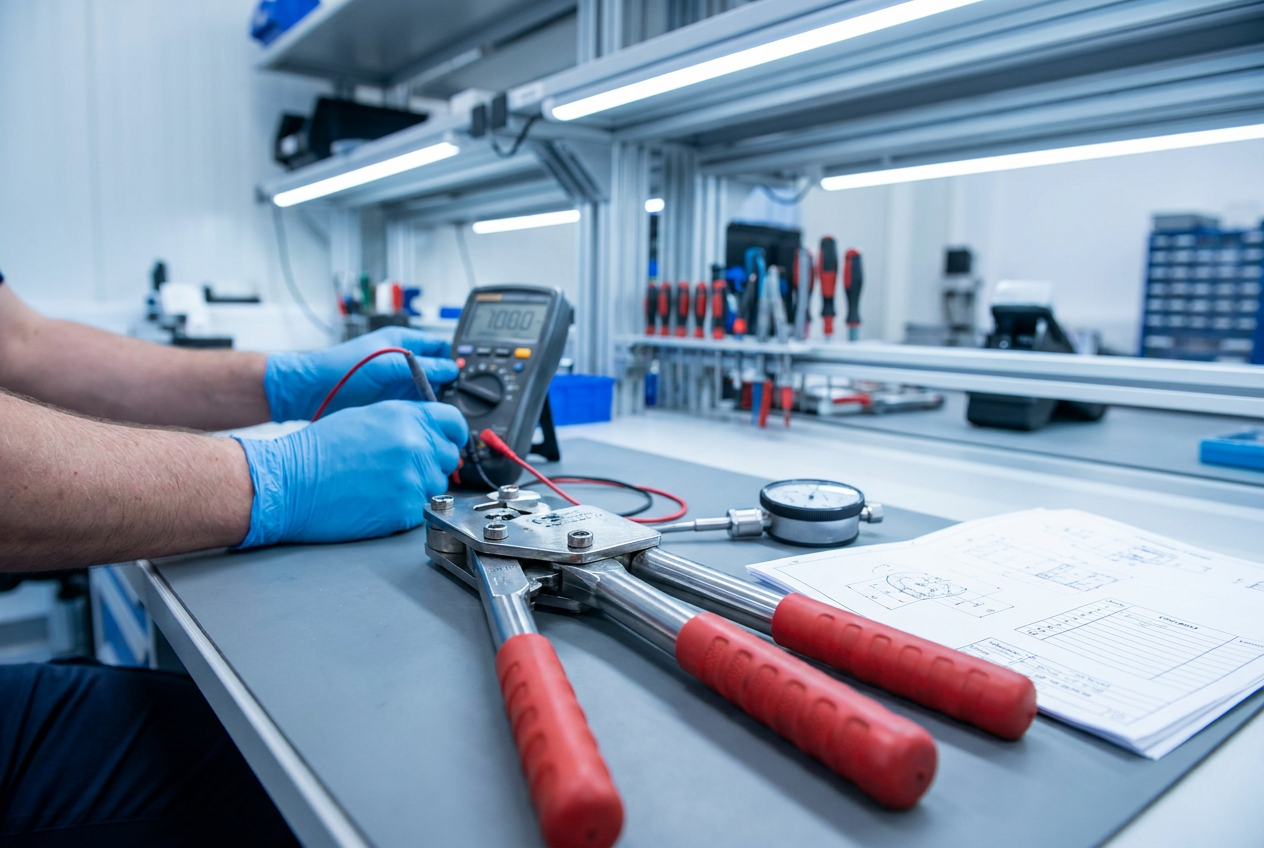
Why Sticker-Based Crimp Tool Calibration Falls Short in Aerospace Audits
A calibration sticker on your pneumatic crimp tool only proves it met tolerances twelve months ago. It tells you nothing about the 15,000 cycles executed since last Tuesday on high-density mil-spec contacts.
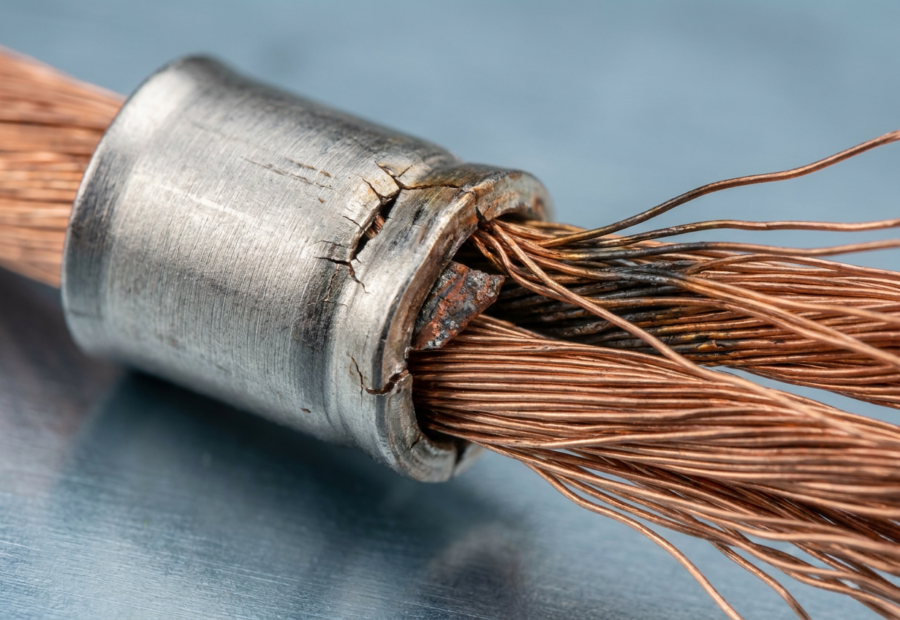
When an FAA auditor inspects your wire harness line, relying on expiration dates invites major non-conformances. Tool frames warp, locator pins wear beyond drawing limits, and internal cycle-control pawls lose tension long before the next scheduled calibration date.
Treat the sticker as a baseline, not a guarantee. To satisfy stringent AS9100 quality demands, your internal audit protocol must cross-examine physical tool performance against actual shop-floor usage data. If your operators cannot trace a finished harness back to a specific die-set verification and pull-test log, that sticker becomes an administrative liability.
Regulatory and Industry Standards That Define Crimp Tool Compliance
Passing an FAA or primes audit requires aligning your tooling program with strict aerospace standards. AS9100 mandates configuration control, but you must look to specific documents to govern your benchtop crimp tools.
SAE AS50861 and MIL-DTL-22522 set the baseline for connector and contact compatibility. Meanwhile, SAE AS81969 governs insertion and removal tool integrity, directly impacting contact retention. Your quality system must map every frame and positioner to these specifications.
During an audit, investigators cross-reference your internal calibration logs with MIL-STD-790 reliability requirements. If your technicians use non-standard hand crimp tools without traceable calibration cycles tied back to NIST standards, you face immediate non-conformance findings. Establishing this compliance framework prevents costly line stoppages and protects flight hardware.
Building a Crimp Tool Compliance Audit Framework: Documentation, Traceability, and Interval Control
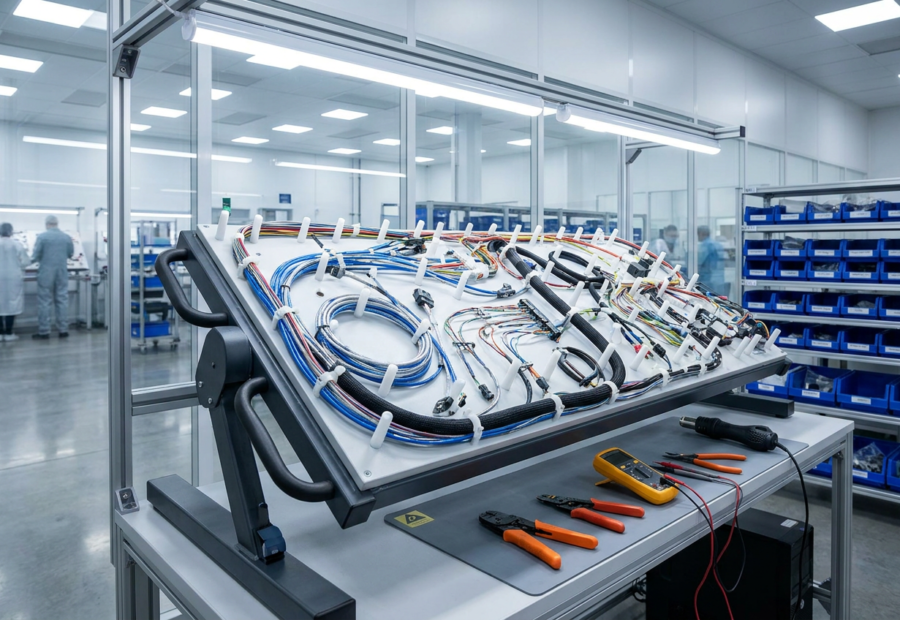
Transitioning from passive sticker reliance to an active crimp tool compliance audit demands a closed-loop system tying every die set to a specific work order. Start by logging unique tool serial numbers directly into your enterprise resource planning software alongside calibration certificates.
Establish interval controls driven by cycle counts rather than static calendar months. For instance, high-use DMC M22520 frame assemblies running in a multi-shift MRO environment require verification every 1,000 cycles, whereas bench-mounted pneumatic presses need daily stroke checks.
| Control Parameter | Minimum Requirement | Audit Verification Target |
|---|---|---|
| Asset ID | Laser-etched on tool frame | 100% physical-to-digital match |
| Cycle Threshold | Manufacturer or engineering limit | Logbook or digital counter audit |
| Traceability | Operator ID tied to harness lot | Forward and backward traceability |
Maintain rigid configuration control so technicians cannot swap locator heads without a documented engineering sign-off.
Beyond Calibration Stickers: Verifying Crimp Tool Performance Through Pull-Off Force Testing and Crimp Height Measurement
Building on your traceability framework, verifying physical tool output closes the compliance gap between shelf-life expiration and operational reality. A valid crimp tool compliance audit requires direct measurement against SAE AS50881 specifications using calibrated micrometers and tensile testers.
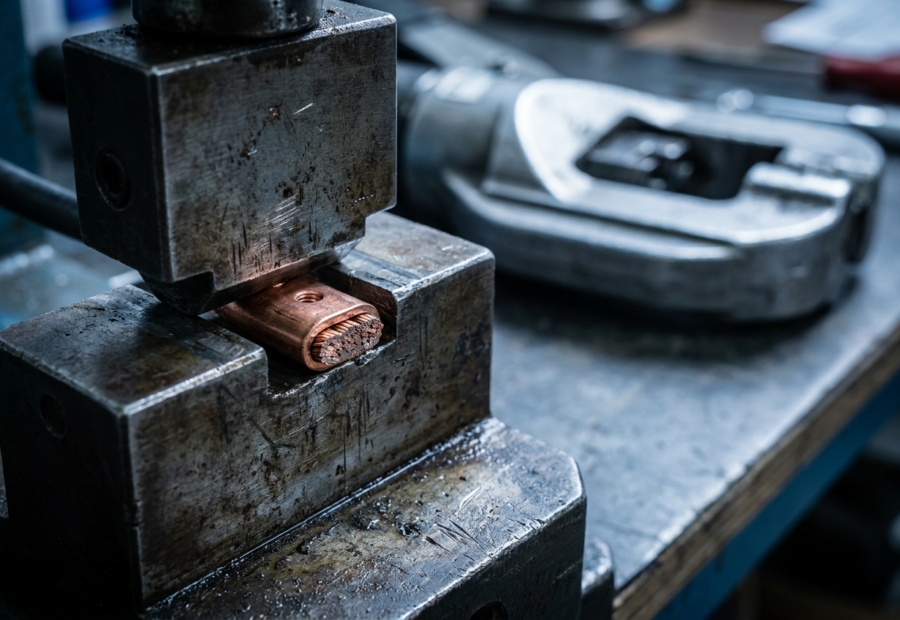
Begin by measuring cross-section crimp height on test samples for every gauge wire run. Compare your micrometer readings directly against the tool manufacturer’s engineering limits—typically a tight tolerance window of ±0.03mm. Next, execute destructive pull-off force testing on a motorized test stand operating at a constant rate of 25mm per minute. If a 20 AWG Mil-Spec contact slips below the 14-pound minimum tensile threshold, quarantine that frame immediately, regardless of its calibration date.
Common Audit Findings and How to Address Them
Auditors frequently flag uncalibrated backup positioners, missing daily verification logs, and worn indenters that pass static gauge checks yet fail tensile pulls. When a quality inspector discovers an expired calibration date on the shop floor, quarantine the asset immediately and pull the last three lots of wire harnesses built with that tool for destructive pull testing.
| Common Audit Finding | Root Cause | Corrective Action |
|---|---|---|
| Expired tool in active production | Lack of automated asset locking | Implement tool crib checkout software tied to calibration status |
| Missing daily verification records | Operator omission or uncollected logs | Mandate digital log sign-offs before the shift starts |
| Worn gaging pins | Improper storage or physical damage | Institute monthly optical comparator inspections for all pin gages |
Checklist: Preparing Your Crimp Tool Program for a Compliance Audit
Execute this four-step verification sequence before your next quality audit to eliminate non-conformances.
- Verify Asset Master Lists: Cross-reference every active hand tool, pneumatic crimper, and die set on your shop floor against the active calibration database to confirm unique serial number tracking.
- Inspect Daily Log Continuity: Audit operator workstations to ensure pull-off force test logs and go/no-go pin gauge measurements are recorded for every shift, with zero skipped entries.
- Audit Out-of-Service Security: Check physical quarantine bins. Every tool flagged for wear or calibration lapse must be locked away, tagged out, and barred from production.
- Review Calibration Certificates: Validate that external lab certificates trace directly to NIST standards and explicitly list the specific jaw gap dimensions tested.
Conclusion: Embedding Crimp Tool Compliance Into Your Quality Culture
Passing your next FAA audit requires shifting your mindset from reactive paper chasing to proactive tool verification. When you treat your crimp tool compliance audit as an ongoing engineering safeguard rather than an annual paperwork drill, you permanently eliminate silent wire harness failures on the shop floor.
Maintain strict calibration intervals, mandate daily pull-off verification logs, and isolate worn indenters immediately upon detection. By locking down these physical variables, you protect your production line from costly scrap and maintain absolute traceability across every delivered flight assembly. Empower your quality technicians to challenge tool readiness at the workstation level today to secure mission-critical reliability tomorrow.
Frequently Asked Questions
Why is relying solely on a calibration sticker insufficient for regulatory reviews?
A physical sticker only indicates past compliance at the moment of testing rather than operational health after thousands of cycles. Auditors demand proof that tools maintain precision under daily production stress. Active verification bridges the gap between annual inspections and real-world wear.
What specific standards govern benchtop tooling programs during an aerospace inspection?
While AS9100 establishes overarching quality management requirements, specific SAE guidelines dictate precise calibration parameters for benchtop crimping equipment. Facilities must align their internal operating procedures with these aerospace directives to satisfy regulatory bodies.
How does asset traceability impact the success of a quality inspection?
Maintaining a closed-loop tracking system connects individual die sets and pneumatic crimpers directly to specific active work orders. This granular tracking enables quality teams to quickly isolate and quarantine potentially defective assemblies if a tool drifts out of tolerance.
What physical tests are necessary to prove mechanical integrity beyond standard gauge checks?
Quality teams utilize pull-off force testing and precise crimp height measurements to evaluate actual physical output. These methods confirm that electrical terminations withstand required mechanical stress despite normal mechanical wear.
How can a facility prevent common audit flags regarding backup positioners?
Shops must include all supporting hardware, such as positioners and interchangeable die sets, within their master calibration tracking system. Treating secondary components with the same rigor as the primary crimp tool prevents critical non-conformances during floor walkthroughs.